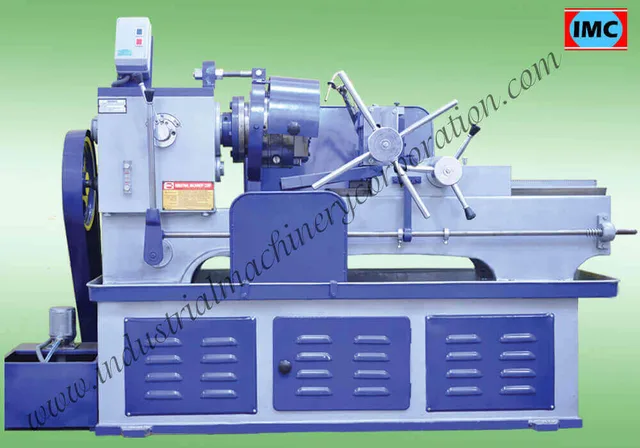
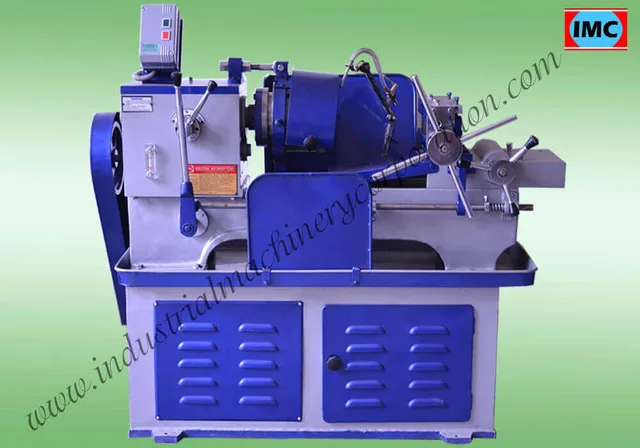
The technical information below is based on the model data stored for this product. Final machine capacity, die-head size, chaser profile and thread result should be confirmed against the actual pipe and required thread standard before order confirmation.
Pipe Threader Working Principle
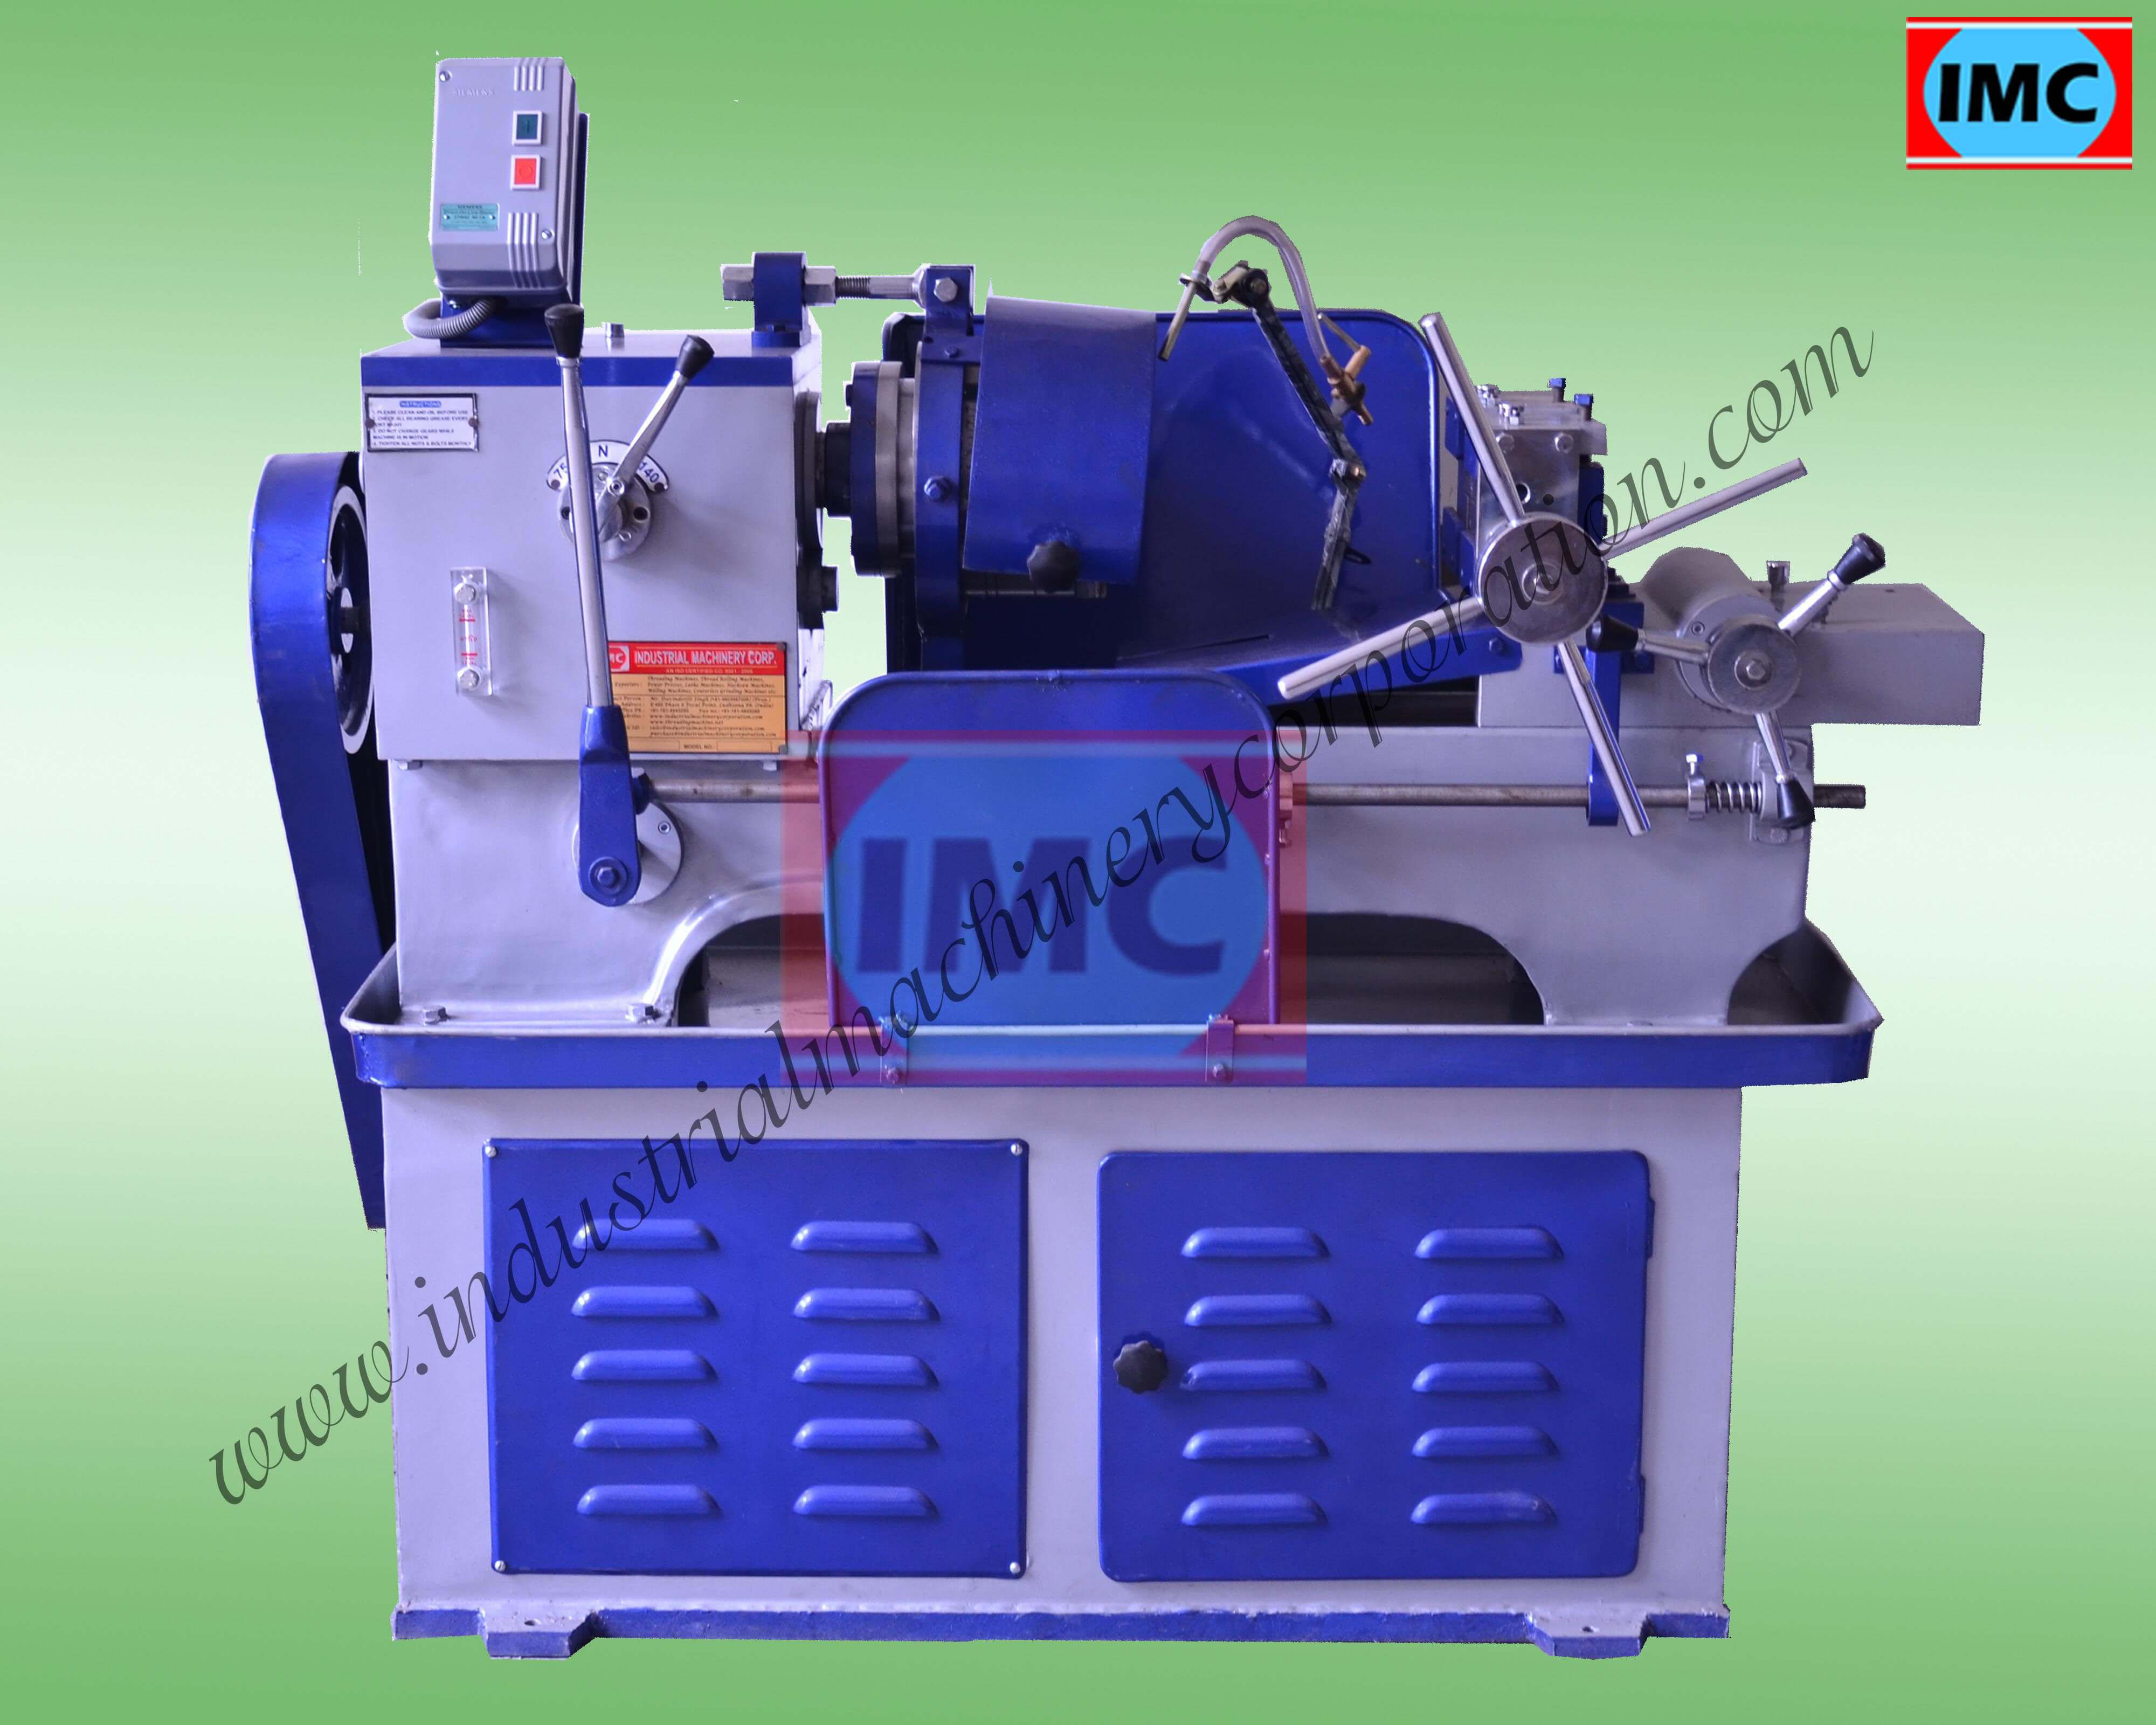
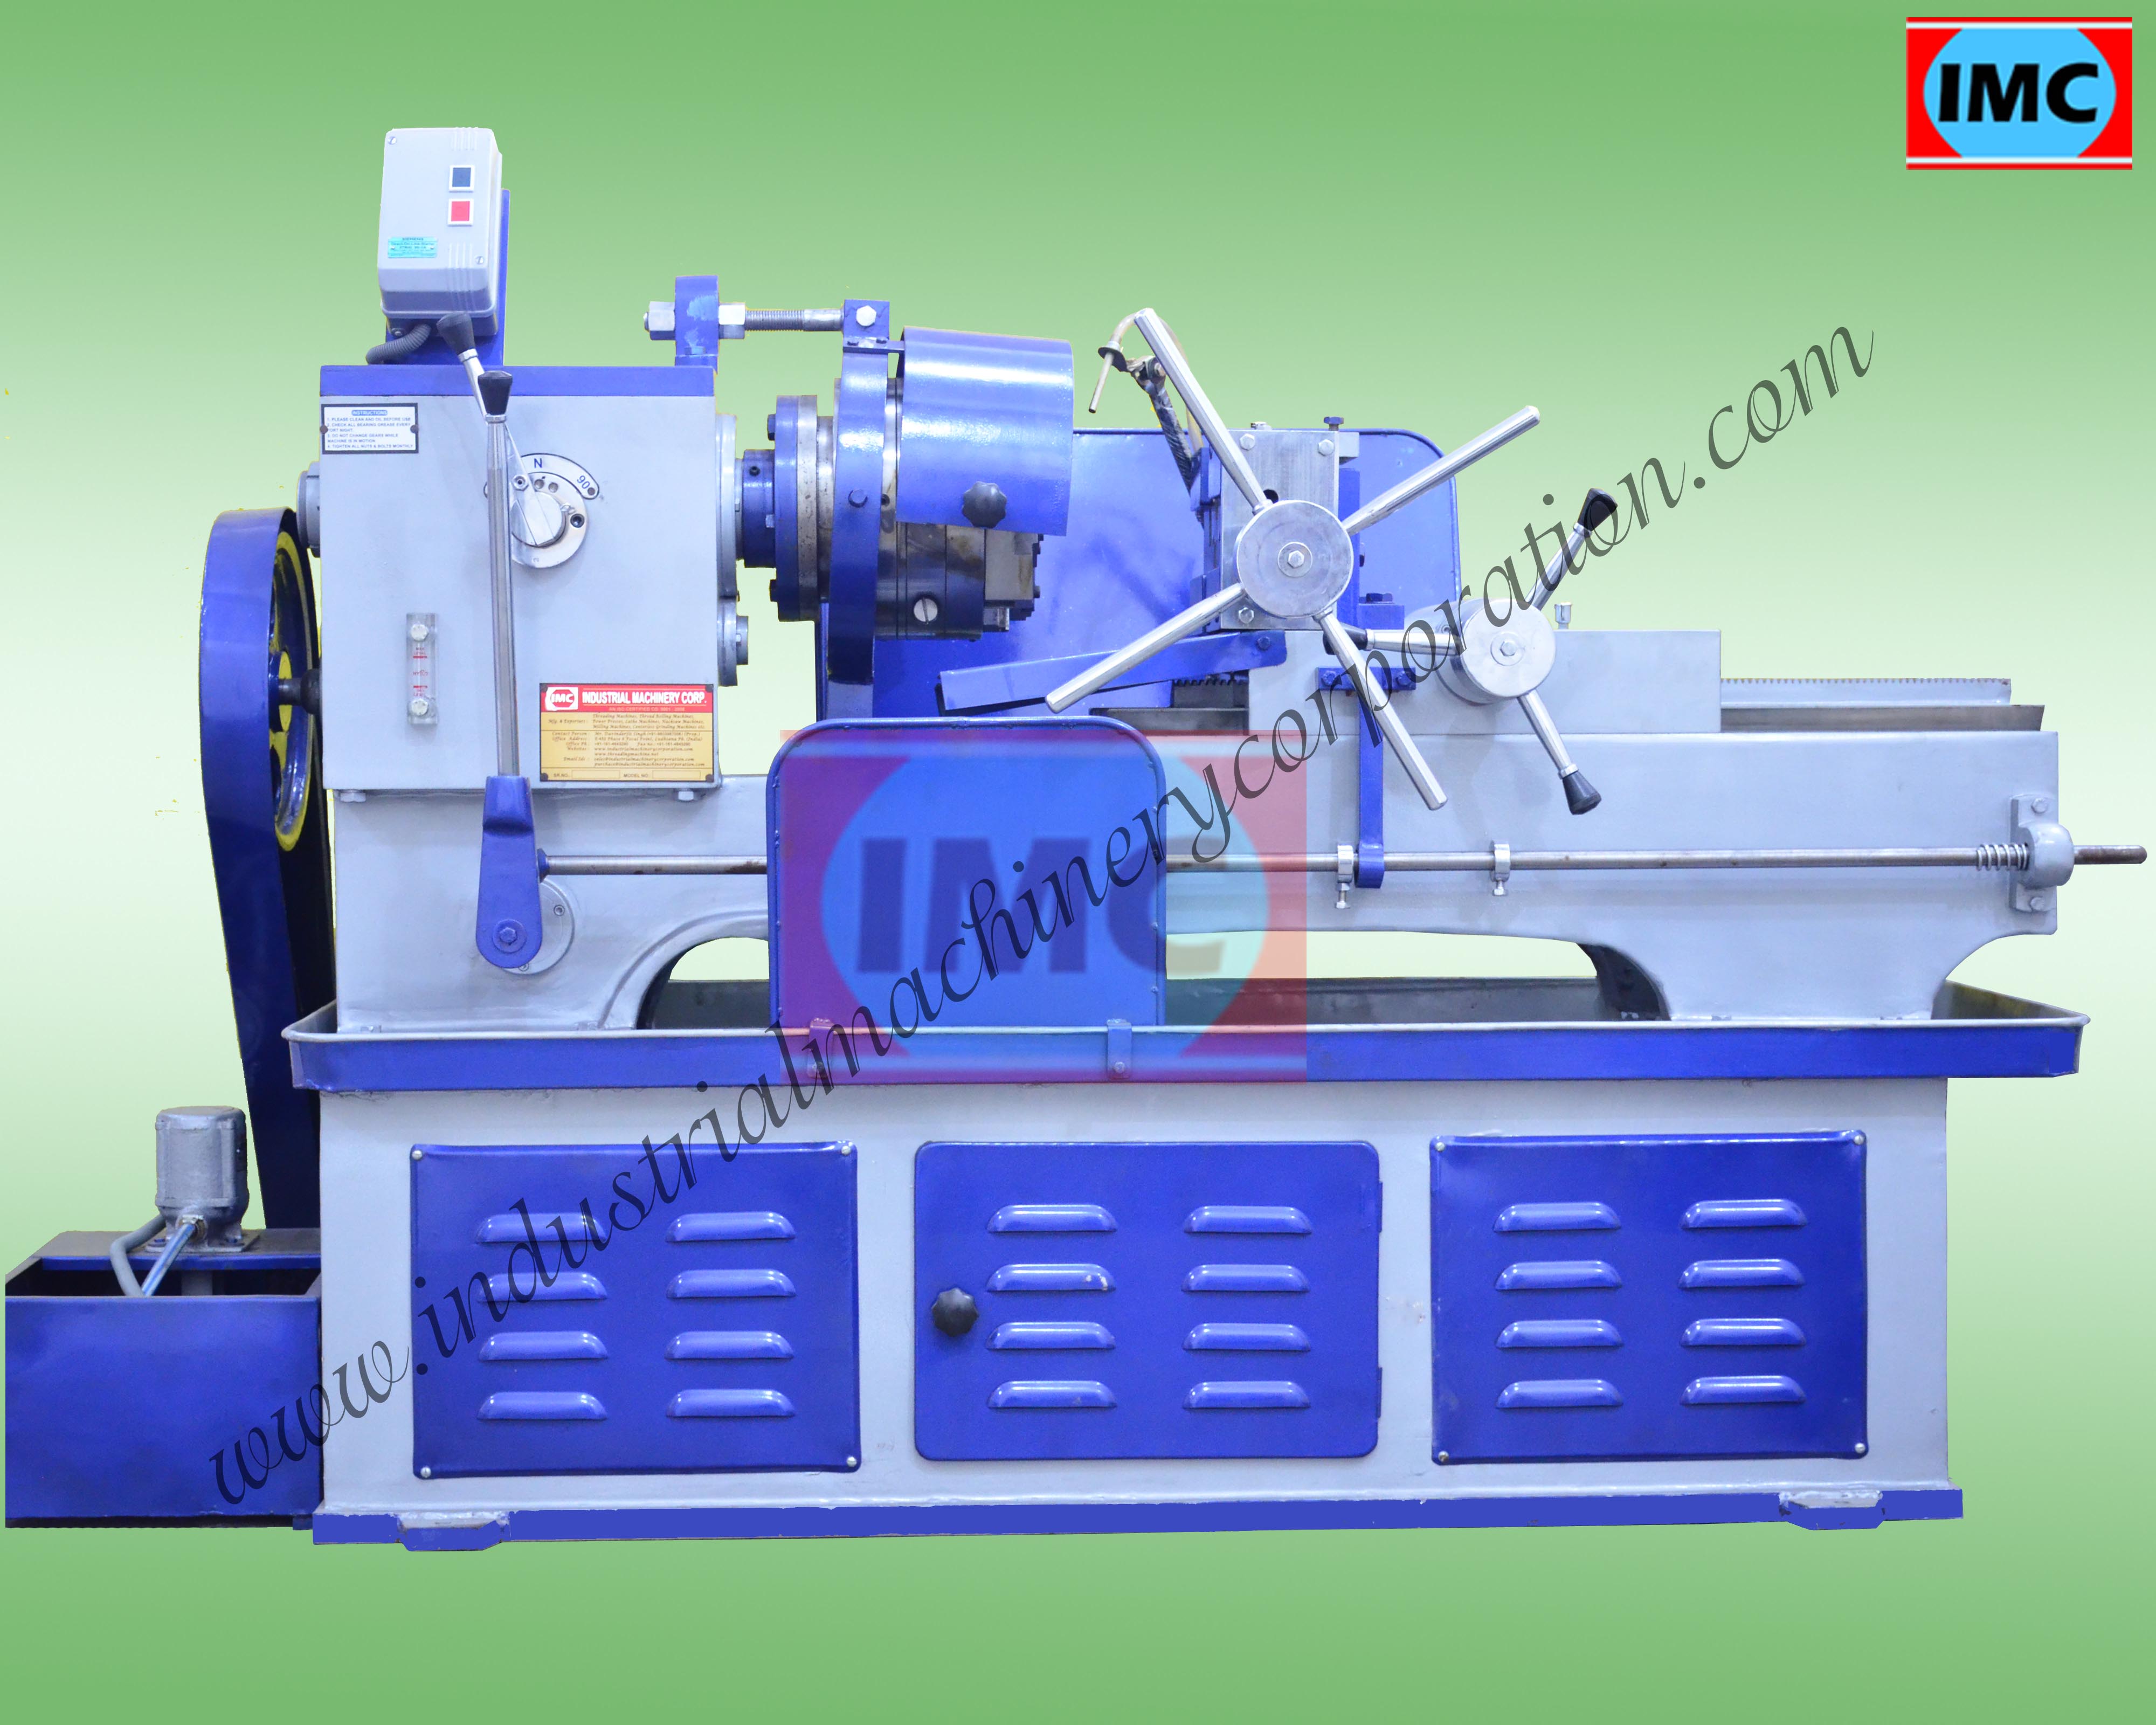
In a chaser-type Pipe Threader, the pipe is held securely in the clamping system while the die head rotates around the job. Suitable tangential chasers remove material progressively to produce the required external thread. The tooling, spindle speed and machine size are selected according to the pipe diameter, material, thread form and thread length.
Bed Type vs Pillar Type Pipe Threader
Bed-type machines are generally selected where the job and tooling arrangement require a rigid machine bed and controlled saddle movement. Pillar-type configurations are used for application-specific pipe or scaffolding work where the clamping and machine layout differ. The correct configuration should be confirmed from the component size, thread length and production requirement.
Parallel & Taper Pipe Threads
The existing product information lists Metric, BSP, BSPT, NPT, UNF, UNC, BSW, ACME and BSF thread forms. Exact availability depends on the selected die head, chaser profile, job diameter and machine configuration. BSPT and NPT taper-thread requirements should be specified clearly when requesting a quotation.
Range of IMC Die Heads
- 1/4" to 1" capacity
- 3/8" to 1.1/2" capacity
- 1/2" to 2.1/2" capacity
- 1" to 4" capacity
- 2.1/2" to 6" capacity
- 4" to 8" capacity
Pipe Threader Models & Technical Specifications
| Specification |
3/8" to 2" (10–50 mm) |
1/2" to 2.1/2" (12–65 mm) |
1" to 4" (25–100 mm) |
2.1/2" to 6" (65–150 mm) |
4" to 8" (100–200 mm) |
8" to 10" (200–250 mm) |
| Saddle Movement | 10"–12" | 16" | 10"–12" | 8" | 8" | 8" |
| Spindle Speed Range | 127–180 | 60–90–120 | 40–75–115 | 25–50 | 25–50 | 10–20–30 |
| Number of Spindle Speeds | 2 | 3 | 3 | 2 | 2 | 3 |
| Threading Capacity | 3/8" to 2" | 1/2" to 3" | 1" to 4" | 2.1/2" to 6" | 4" to 8" | 8" to 10" |
| Production per Hour | 100–120 | 70–90 | 35–40 | 20–25 | 15–20 | 15–20 |
| H.P. Required | 3 H.P. | 7.5 H.P. | 12.5 H.P. 960 | 15 H.P. 960 | 20 H.P. 960 | 30 H.P. 960 |
| Lead Screw | Provided | Provided | Provided | Provided | Provided | Provided |
| Weight (Approx.) | 550 kg | 990 kg | 1600 kg | 1900 kg | 2500 kg | 5000 kg |
Machine Selection Notes
For a 1" to 4" pipe-threading application, the stored model data lists a spindle-speed range of 40–75–115, three spindle speeds, indicated production of 35–40 pieces per hour, lead screw provided and approximate machine weight of 1600 kg. Actual output depends on pipe material, thread length, tooling and operator setup.
Spindle-speed clarification: The published spindle-speed row does not state its unit. Confirm the unit and available speeds for the selected configuration with IMC.